Resources
Thermal break in window profiles — what to specify
Published 2026-09-01
Almost every window enquiry that reaches us says either "thermal break" or "no thermal break", and almost none of them say anything else about it. That is understandable — from the buying side it looks like a material choice, a box to tick. It is not. A thermal break is a joint between two separate extrusions, and everything that goes wrong with it goes wrong at that joint. This is what we would want a buyer to understand before comparing two quotes that both say the same two words.
It is an assembly, not a material
Most people picture the thermal break as the bar of low-conductivity material — usually polyamide — sitting between the inside and the outside of the frame. That bar is real, but it is not what you are buying. You are buying a joint: two aluminium sections extruded separately, each with a groove designed to receive the bar; the bars inserted; and then the aluminium mechanically rolled over onto them so that three loose pieces behave as one structural member.
That reframing has a commercial consequence. The polyamide is the cheapest part of the assembly. What decides whether the composite bar actually performs is the die work that produced the grooves and the rolling operation that closed them — neither of which appears anywhere on a quotation.
So when a thermal-break profile is quoted noticeably cheaper than the others, the strip is almost never where the money was saved.
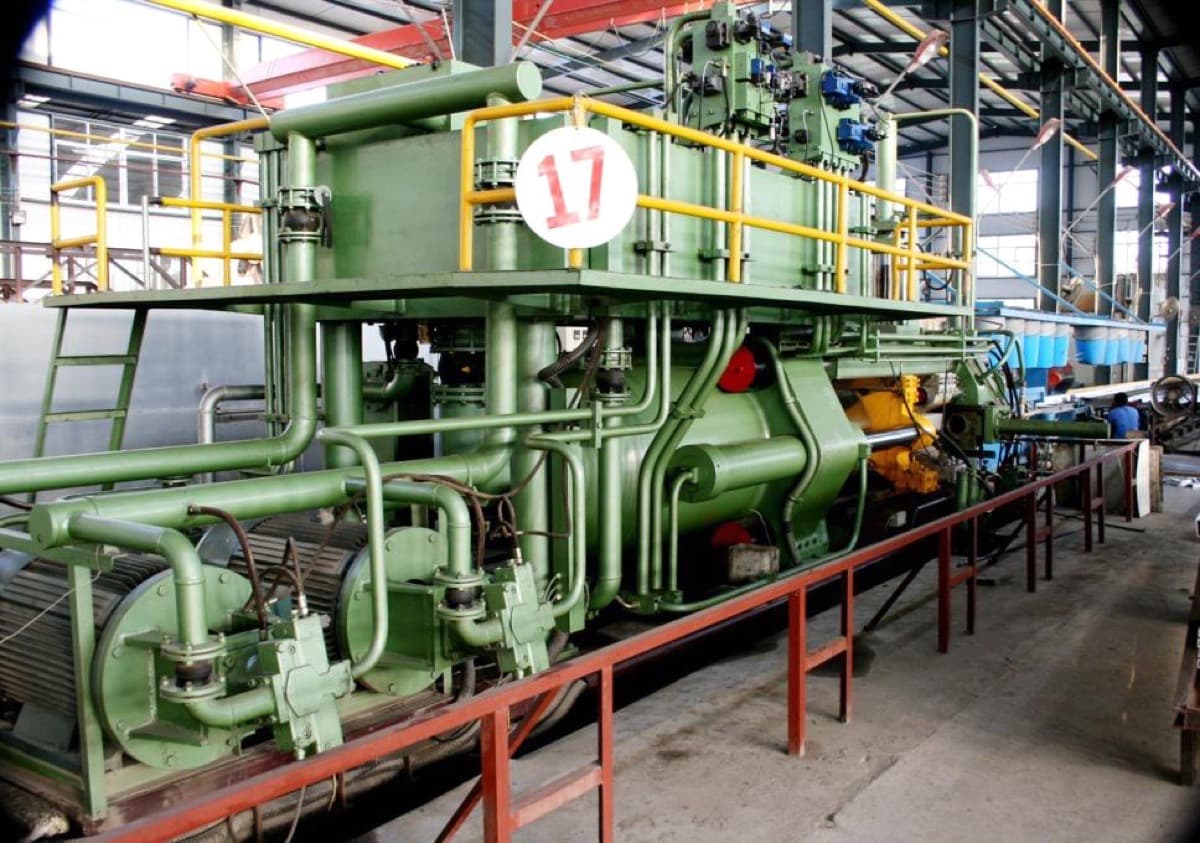
Two dies, and they have to be drawn for each other
A broken profile is two profiles. Two sections, two dies, two sets of sampling and correction before either one runs clean. That is worth knowing before you put a broken quote next to a solid one and read the difference as margin — a meaningful part of it is tooling that genuinely exists twice.
The grooves are the most demanding features on the whole section. Elsewhere on a window profile, a small deviation is cosmetic or gets taken up by a gasket. On the groove it decides whether the bar seats properly and whether the rolling grips it. We extrude to EN 12020, but on this one feature the general tolerance is not where the conversation should end — if the system designer has a view on the groove, it belongs on the drawing.
And a thermal break cannot be added later to a section that was not drawn for one. It is a new pair of dies, not a modification of an existing one. If you are moving an existing window system from solid to broken, budget it as new tooling and a new sampling cycle, because that is what it is.
What goes wrong is the rolling, not the polyamide
The bar itself rarely fails as a material. The failures that come back are joint failures. Rolled too lightly, the bar can creep or slide within the groove, usually showing up first at the cut ends. Rolled too hard, the aluminium deforms — the profile bows, or the groove lip is damaged and grips less than it looks like it does.
On site the symptom is not "the thermal break failed". It is a sash that will not stay square, a corner crimp that does not close, or two halves visibly offset from each other at a cut end. If you want a quick check on delivery, look at the ends of a few bars: the bars should be flush and tight, not standing proud and not withdrawn into the groove.
The property that matters here is shear — the composite bar only carries load as a single member while the joint resists the two halves sliding relative to each other. There is a standard test for exactly this. We would rather you asked what a supplier does to verify it, and what they can actually show you, than took the words "thermal break" on a quotation at face value.
Heat, and colour, after the bar is assembled
Polyamide has a working temperature limit, and a powder curing oven is hot. The normal sequence is therefore to finish the two halves first and assemble afterwards. If a supplier is coating after assembly, that is a question worth asking rather than an automatic fault — but it should be a deliberate answer, not a surprise.
Anodizing effectively forces the order. It is an electrochemical process that needs current through the part, and an assembled composite bar has a non-conductive layer running down the middle of it. In practice the halves are anodized as separate profiles and joined after. Worth knowing if your specification names an anodized finish and you were imagining a single assembled bar going into the tank.
Colour has a consequence people meet on site rather than on paper. A dark exterior face in strong sun sits at a very different temperature from the shaded interior face, the two halves want to expand by different amounts, and a long composite member responds by bowing. It is not a defect in the bar; it is physics working on a member made of two things at two temperatures. Tell us the exterior colour and the bar length together — those two facts belong in the same sentence.
When you should not buy one
In a warm, dry climate with no heating season and no condensation requirement, a solid section can be entirely adequate and costs meaningfully less. Choosing it is a legitimate engineering decision, not a downgrade, and we would rather say so than sell an assembly the project does not need.
The frame is also only part of the opening. If the thermal performance of the window is being held back by the glazing unit, a broken frame will not rescue it — that is money placed where it does the least. A broken frame around a single pane is the clearest version of that mistake, and we have seen it specified.
Where an energy code applies, where condensation on the inside face is a stated requirement, or where there is a real heating and cooling load behind the wall, it stops being optional. That call belongs to whoever is specifying the project, not to the extruder. What we need from you is simply which of the two situations you are in.
What to send with the enquiry
Say whether the specification calls for a thermal break at all, and if the window system is already designed, send the section drawing. Running an existing, proven pair of dies is faster, cheaper and far less risky than redesigning the section from scratch.
Say what the finish is and when it is applied relative to assembly, so nobody has to assume. Say the bar length and the exterior colour together.
Say whether you want the composite bar delivered assembled, or the two halves loose. Assembled is the normal case, but some fabricators roll the bars in their own plant — if that is you, say it at enquiry stage, because it changes what we need to hold on the grooves.
And if you genuinely do not know whether this project needs a break, send us the drawing and the location. That is a five-minute conversation before tooling, and an expensive one afterwards.
Related
Profiles in this guide